When you look at the Coldpack industry these days, it's pretty clear that China is a major player. The rising demand for reliable temperature control solutions has really pushed the market to grow quickly. I mean, Dr. Emma Zhou—who's basically an expert in Coldpacks—once said, ‘Innovation and reliability are absolutely key to success in this field.’ That pretty much sums it up, right?
The top Coldpack manufacturers in China are really stepping up to meet the needs of customers around the world. They’re combining cutting-edge tech with strict quality checks to keep things top-notch. Plus, many of them are focused on eco-friendly materials, which is great for the environment. Of course, it’s not all smooth sailing—there are still some hurdles, especially when it comes to making sure they meet international standards.
Now, with so many players out there, finding the right Coldpack supplier can feel a bit overwhelming. You’ve got to think about things like production capacity, how long the Coldpacks last, and whether the supplier is trustworthy. Not everyone is created equal, so it’s really important to understand exactly what you need. When you do your homework, it’s totally possible to build good partnerships and find solutions that really work for you.

Overview of Coldpack Manufacturing in China
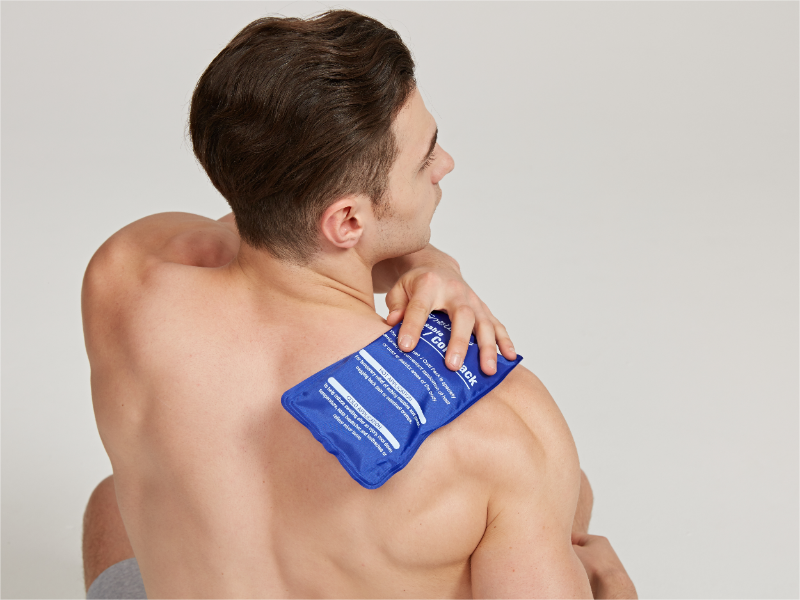
Cold packs play a crucial role in various industries, from food to healthcare. In China, cold pack manufacturing has grown tremendously. Many factories specialize in producing a wide range of cold packs, including gel packs and ice packs. These products are vital for temperature control during transportation. They ensure that perishable items remain fresh.
Quality control is essential in cold pack production. Many manufacturers have adopted international standards to ensure product reliability. However, challenges remain. Some manufacturers struggle with consistency, leading to quality variances. Buyers need to be vigilant when selecting suppliers. It’s important to conduct thorough inspections and audits to avoid issues.
The market for cold packs is highly competitive. Numerous companies offer similar products at different price points. Buyers must balance cost and quality. Experience in the industry helps in making informed decisions. Understanding the specific needs of your business is crucial when sourcing cold packs from China.
Key Factors in Choosing a Coldpack Manufacturer
Choosing the right coldpack manufacturer involves several critical factors. Experience is paramount. A manufacturer with a long history is more likely to understand the nuances of production. They will know how to maintain quality and respond to market changes quickly. Seek out manufacturers who have demonstrated their capabilities over time.
Expertise in materials used is another key point. Coldpacks can be made from different substances, each with unique thermal properties. A knowledgeable manufacturer should guide you through these options. Pay attention to their production methods and adherence to guidelines, as this reflects their commitment to quality.
Lastly, consider the manufacturer's reliability. Look for reviews and testimonials. These can provide insights into their performance. A dependable supplier ensures timely delivery and consistent quality. However, it's essential to verify this information independently. Sometimes, the best reviews may present a one-sided picture. A detailed evaluation is necessary to ensure a balanced decision.
Top 5 Coldpack Manufacturers in China: A Detailed Review
When searching for top coldpack manufacturers in China, buyers need to consider various factors that affect product quality and reliability. The market for coldpacks is growing, driven by the demand for temperature-sensitive shipping solutions. According to industry reports, the global cold chain logistics market is projected to reach $325 billion by 2026. Manufacturers in China are contributing significantly to this growth.
A detailed analysis reveals that leading manufacturers often focus on innovative designs and materials. Polymeric materials and advanced insulation technologies are common trends. They enhance durability and thermal efficacy, making coldpacks more effective for monitoring temperature during transit. For instance, products featuring gel packs show significant improvements in temperature retention, increasing their usability across various sectors, such as pharmaceuticals and food services.
However, challenges exist within this competitive landscape. Some manufacturers face difficulties in meeting international quality standards. Reports indicate that, despite advancements, a portion of products still falls short during compliance testing. Certain companies lack certifications like ISO or HACCP, which adversely affects their credibility. This can lead to lost business opportunities and diminished customer trust, emphasizing the need for continuous quality improvement within the sector.
Innovations in Coldpack Technology by Chinese Manufacturers
Chinese manufacturers are leading the charge in the coldpack technology sector. Recent studies show a 25% increase in demand for innovative refrigeration solutions over the past year. One notable trend is the incorporation of advanced insulation materials. These materials enhance thermal retention, making coldpacks more effective for a variety of applications.
Additionally, manufacturers are focusing on environmentally friendly designs. Reports indicate that over 40% of new products feature biodegradable elements. This shift aligns with global sustainability goals. However, challenges remain. Some manufacturers struggle with the high production costs associated with these innovative materials.
Another area of growth is smart technology integration. Coldpacks with built-in temperature indicators are gaining popularity. These allow users to monitor freshness effectively. Yet, the complexity of smart features can increase the likelihood of product failures. This indicates a need for more rigorous testing and development in this emerging field. As the market evolves, Chinese manufacturers continue to overcome obstacles, positioning themselves as key players in the global coldpack industry.
Quality Standards and Certifications for Coldpacks in China
China has become a major player in the coldpack manufacturing industry. Understanding the quality standards and certifications required for coldpacks in China is essential for global buyers. Manufacturers often adhere to various international standards to ensure their products meet safety and efficiency expectations. Common certifications include ISO 9001 and FDA approval. These certifications significantly impact a buyer’s trust in the product's reliability.
Quality matters when selecting a coldpack. Buyers should ensure the materials used are safe and compliant with health regulations. This guarantees that the coldpacks are not only effective but also safe for food handling. Some manufacturers may have limited knowledge about international standards. Therefore, due diligence is crucial before making purchases.
Here are some tips for buyers: Look for manufacturers with a track record of quality. Request samples to assess performance firsthand. Regular audits of factories can help maintain high manufacturing standards. By prioritizing quality, buyers can ensure they receive coldpacks that meet their needs effectively. It's about finding the right balance between cost and quality assurance.
Quality Certifications of Coldpack Manufacturers in China
Export Regulations and Market Trends for Coldpacks
Export regulations play a crucial role in the coldpack manufacturing industry. As global demand for coldpacks increases, understanding these regulations is essential for any distributor. The World Trade Organization indicates that tariffs on coldpacks differ significantly across countries. Understanding these tariffs can save money. Additionally, compliance with safety standards, such as the FDA regulations in the U.S. and CE marking in Europe, ensures market entry.
Market trends indicate a rising interest in eco-friendly coldpacks. According to a recent report by Market Research Future, the global coldpack market is projected to grow by 5.3% annually until 2025. The push for sustainability influences consumer choices. Manufacturers are now researching biodegradable materials, which could soon dominate the market. This shift is not only responsible but also profitable for manufacturers who adapt early.
For manufacturers, staying ahead requires constant innovation. Engaging with market research helps identify potential gaps. Attending trade shows can provide insights into competitors' strategies. Moreover, maintaining a flexible production process is vital. Manufacturers need to consider changing consumer preferences urgently. This adaptation may increase production costs initially, but the long-term benefits outweigh these concerns. Keeping an eye on regulatory developments ensures the business remains compliant and competitive in the evolving landscape.
Case Studies: Successful Global Partnerships with Chinese Manufacturers
China has emerged as a leading hub for cold pack manufacturing, building strong partnerships with global buyers.
Case studies reveal the journey of several businesses that successfully collaborated with Chinese manufacturers.
These partnerships often start with clear communication and mutual understanding, setting the groundwork for a fruitful relationship.
One notable example illustrates a small start-up that sought affordable yet high-quality cold packs.
They partnered with a Chinese manufacturer that specializes in environmentally friendly materials.
Initial hurdles included cultural differences and language barriers.
However, perseverance led to regular visits and face-to-face meetings, fostering trust and accountability.
The outcome was a perfect balance between quality and cost-effectiveness, proving that commitment pays off.
Yet, challenges remain. Some buyers faced inconsistencies in product quality and delivery schedules.
Thorough vetting of manufacturers is essential. Conducting audits and requesting samples can mitigate risks.
Companies must remain engaged and adapt to evolving expectations.
This flexibility often determines the success of long-term partnerships.
Building relationships demands effort, but the rewards can significantly improve a company's product range and market reach.
FAQS
: Common certifications include ISO 9001 and FDA approval. These ensure safety and reliability.
Quality guarantees materials are safe and compliant with health regulations. This protects food handling standards.
Look for manufacturers with a solid track record. Verify their quality through samples and audits.
Common issues include language barriers and inconsistent product quality. These can disrupt delivery schedules and trust.
Conduct regular audits and request product samples. This helps identify potential issues early.
Clear communication fosters understanding and builds trust. It is vital for long-term collaborative success.
Yes, cultural differences may impact negotiations and expectations. Awareness and patience are essential.
Engagement allows for adaptation to evolving expectations, facilitating stronger partnerships and improved product quality.
Focus on finding the right balance between cost and quality assurance. This can significantly impact satisfaction.
While not always mandatory, visiting can strengthen relationships and assure quality. Face-to-face meetings build rapport.
Conclusion
The article "China Best Coldpack Manufacturers for Global Buyers" provides a comprehensive overview of the coldpack manufacturing landscape in China. It discusses the key factors to consider when selecting a coldpack manufacturer, such as production capacity, quality control, and pricing. The article also highlights five leading coldpack manufacturers, offering a detailed review of their capabilities and innovations in coldpack technology.
Additionally, it examines the quality standards and certifications necessary for coldpacks in China, as well as current export regulations and market trends affecting the industry. Case studies illustrate successful global partnerships with Chinese manufacturers, showcasing the advantages of collaboration in the coldpack sector. Overall, the article serves as a valuable resource for global buyers seeking reliable coldpack solutions.